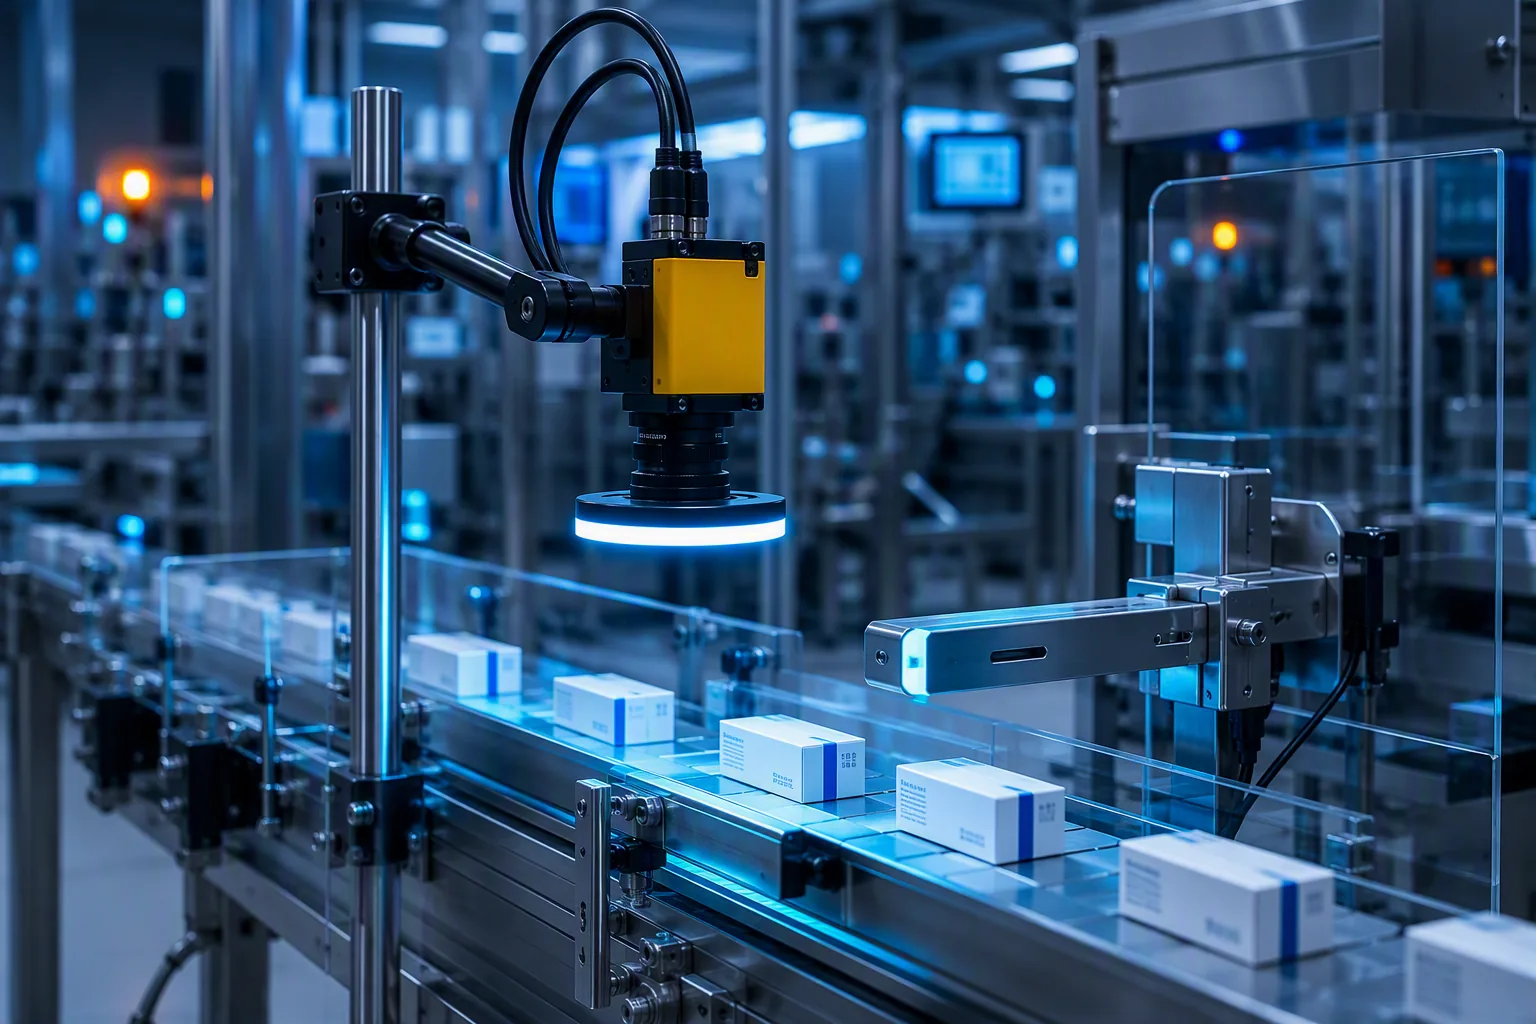
AI-Powered Vision Systems, Intelligent Inspection & Vision-Guided Robotics
As a reliable AI machine vision integrator, we design, deploy, and integrate AI automated optical inspection systems, vision guided robotics, and industrial AI machine vision solutions — all with Artificial Intelligence Software that delivers real-world solutions to the most demanding applications.
Why Manufacturers Need a Machine Vision Integrator
Manual visual inspection is inherently inconsistent — human operators fatigue, miss subtle defects, and cannot sustain the speed required for modern production lines. As quality standards tighten and regulatory requirements increase, relying on human eyes alone creates unacceptable risk.
Industrial machine vision systems inspect every unit at production speed with repeatable accuracy. But automated optical inspection only delivers results when properly integrated with your line controls, lighting, optics, and data infrastructure. That's where an experienced machine vision integrator makes the difference.
Inconsistent quality checks causing defective products to reach customers
Operator fatigue leading to missed defects during long production shifts
Inability to inspect 100% of production at line speed
Regulatory compliance gaps in serialization and traceability
Deep Learning and AI Vision Applications We Integrate
AI Deep Learning Capabilities
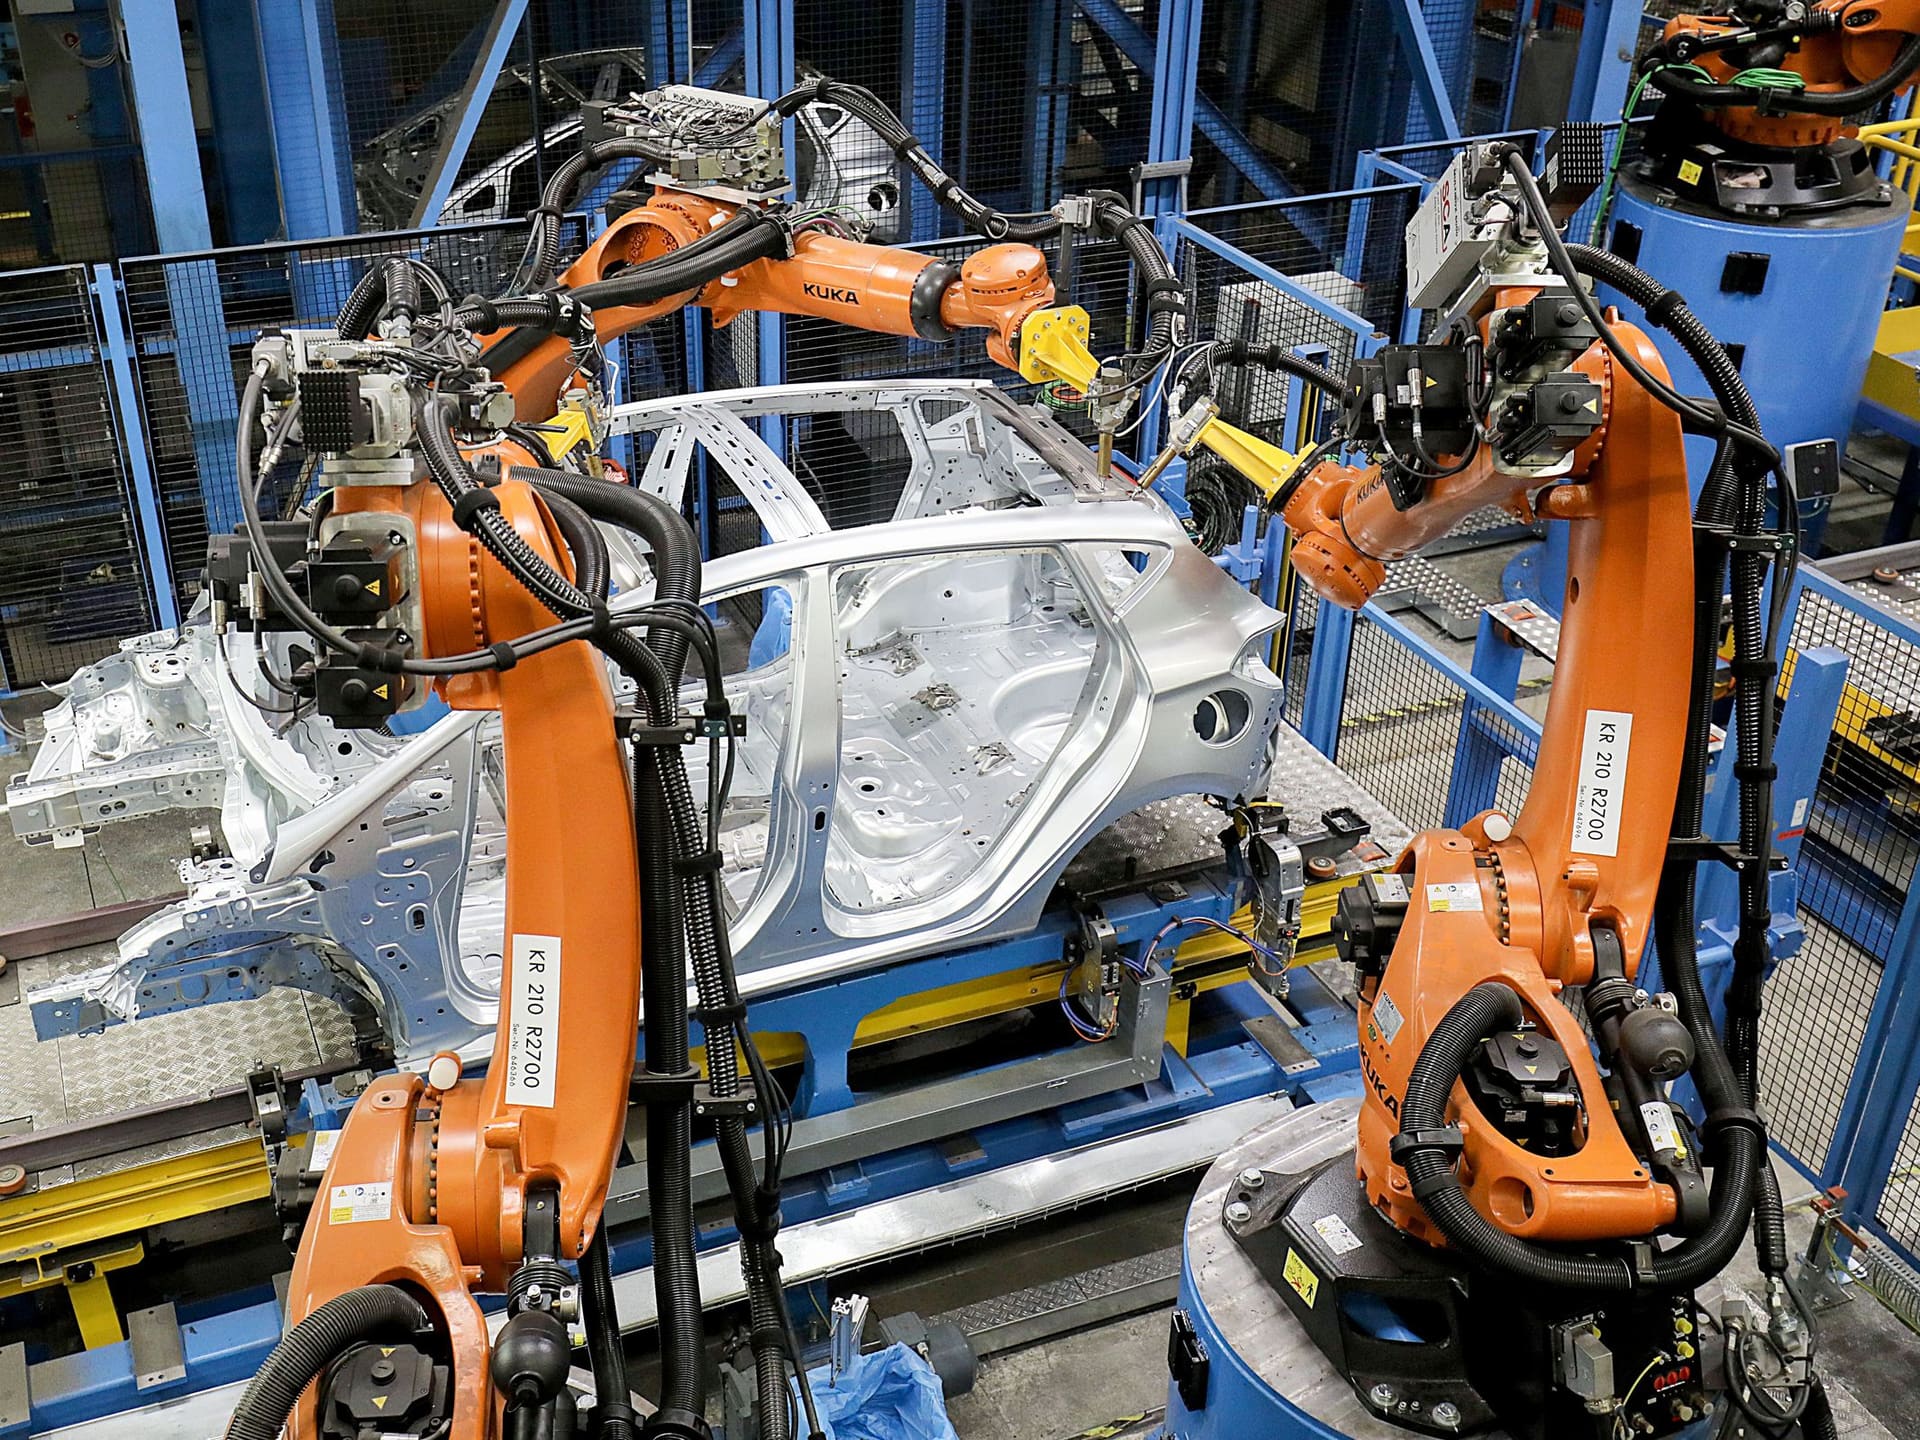
Anomaly Detect
Train the model using only "good" images — no defect samples needed — to automatically identify anomalies and defects. This unsupervised approach eliminates the months of defect-sample collection traditional systems require, making it ideal for products with rare or unpredictable failure modes. The model continuously refines its understanding of "normal" as production data accumulates, catching subtle deviations human inspectors would miss.
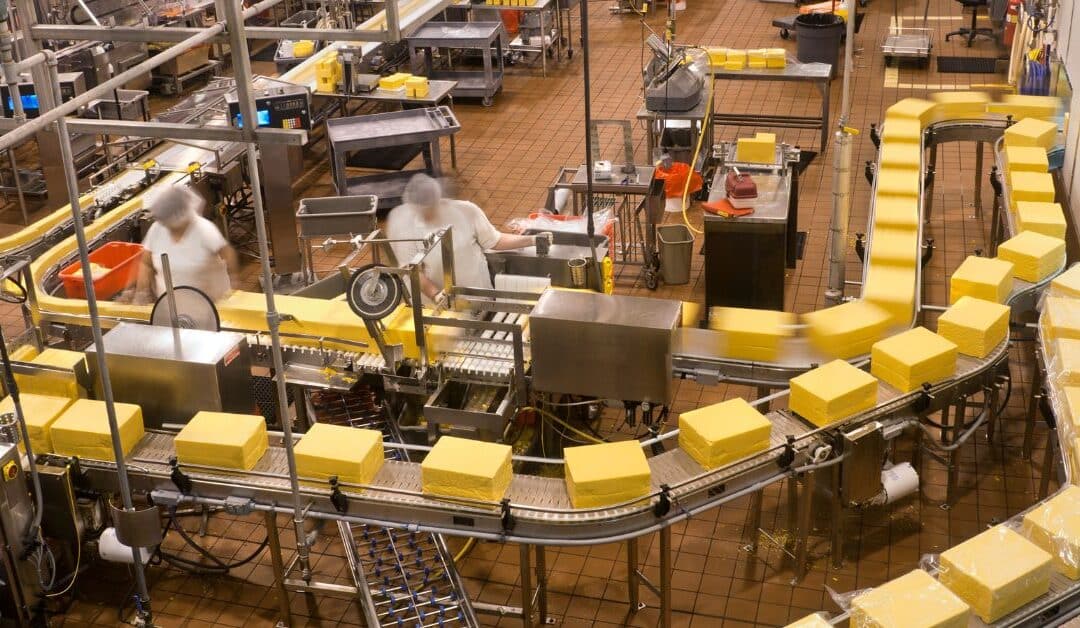
Segment
Isolate and separate key areas of an image for exact, pixel-level analysis. Deep learning segmentation distinguishes overlapping parts, irregular shapes, and complex textures that traditional blob detection cannot separate, giving downstream measurement and defect-detection algorithms a clean, accurately bounded region to analyze — critical for weld bead profiling, fill-level detection, and food product sorting.
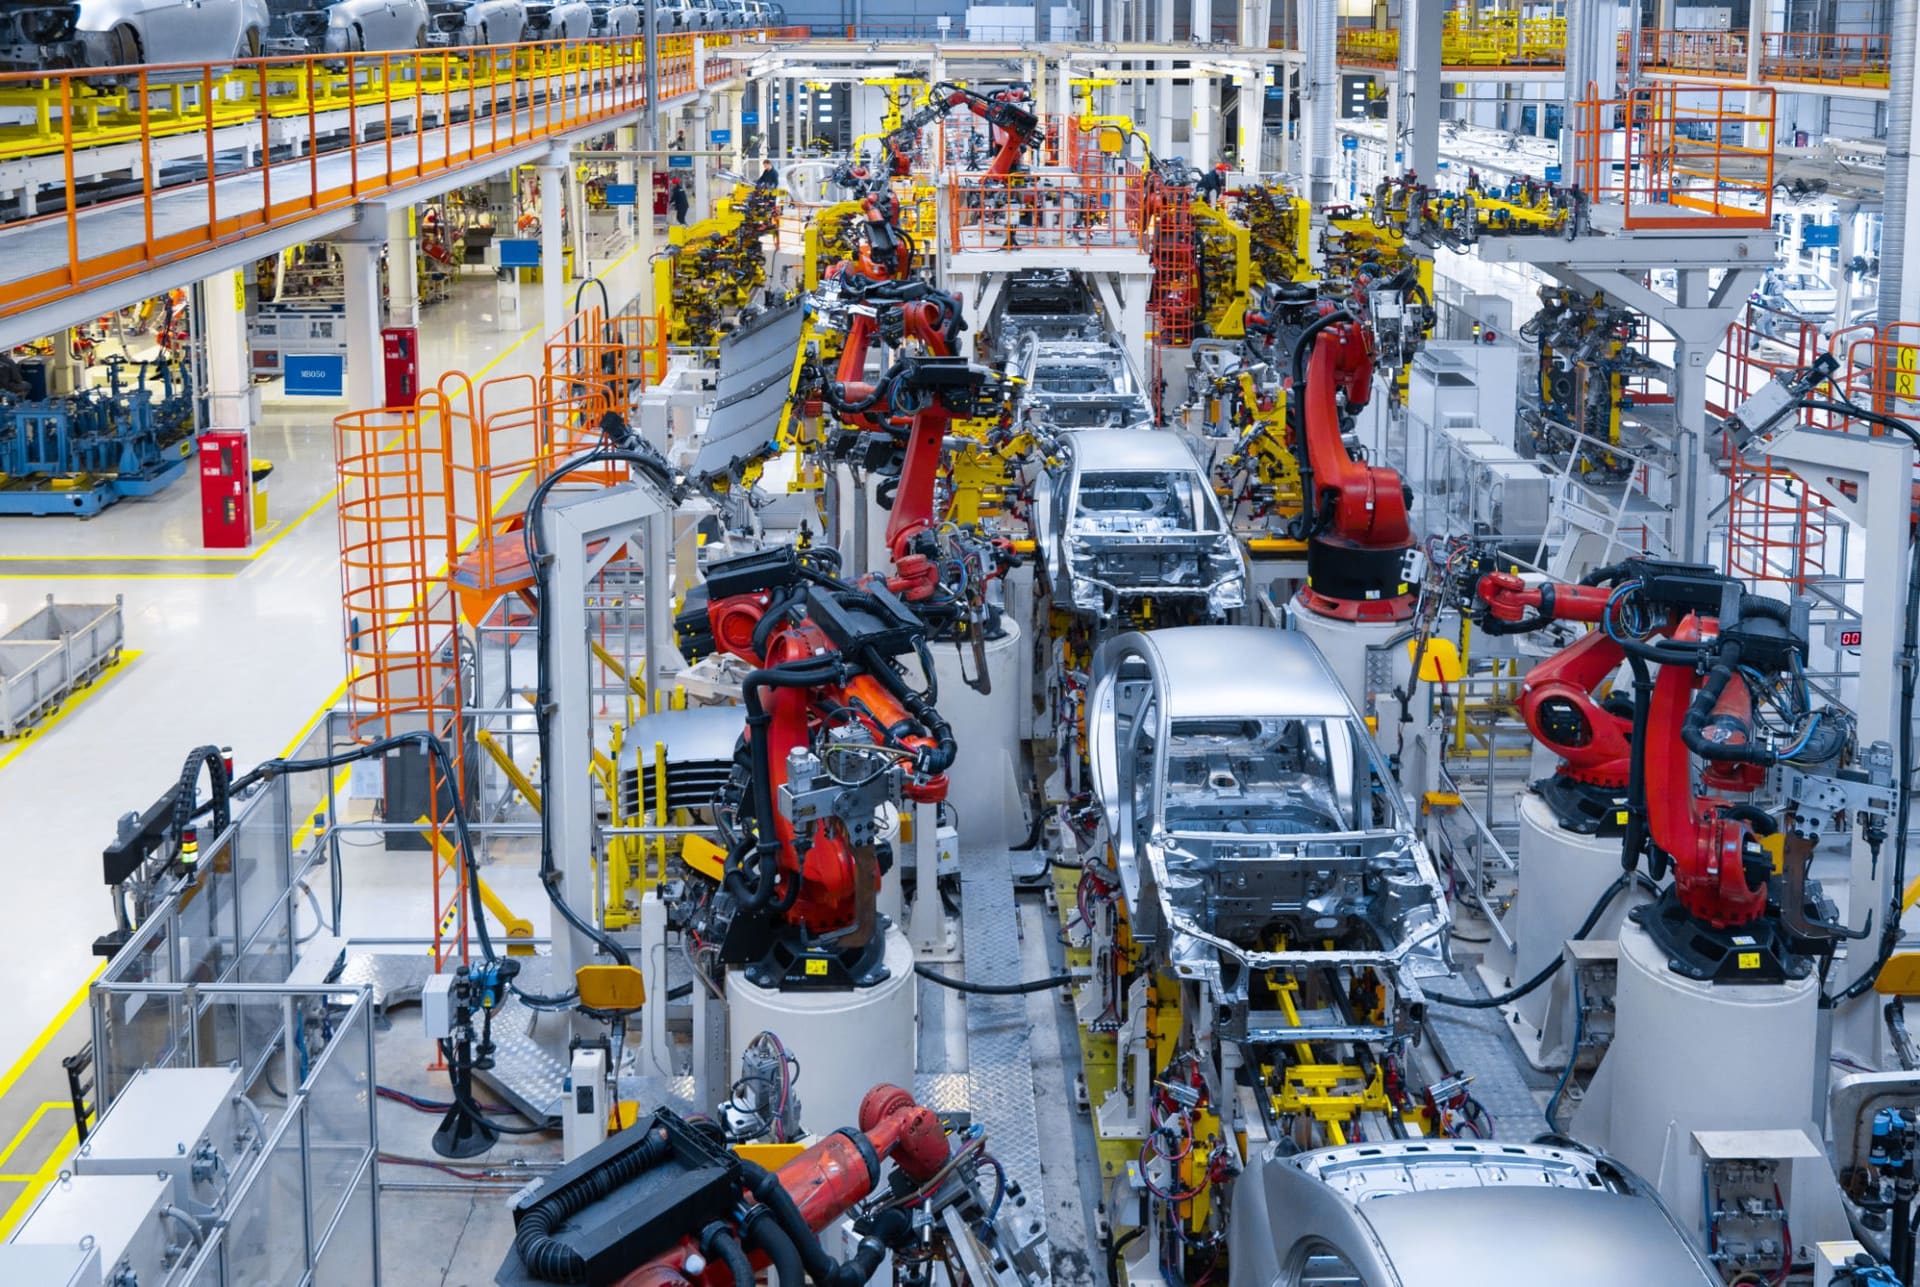
Classify
Identify and categorize parts, defects, or features with high accuracy. Trained on thousands of labeled examples, our classification models distinguish between dozens of part variants, defect types, or material grades in milliseconds — even when visual differences are subtle enough to challenge experienced human inspectors. Confidence scoring flags uncertain cases for review instead of forcing a binary pass/fail call.

Locate
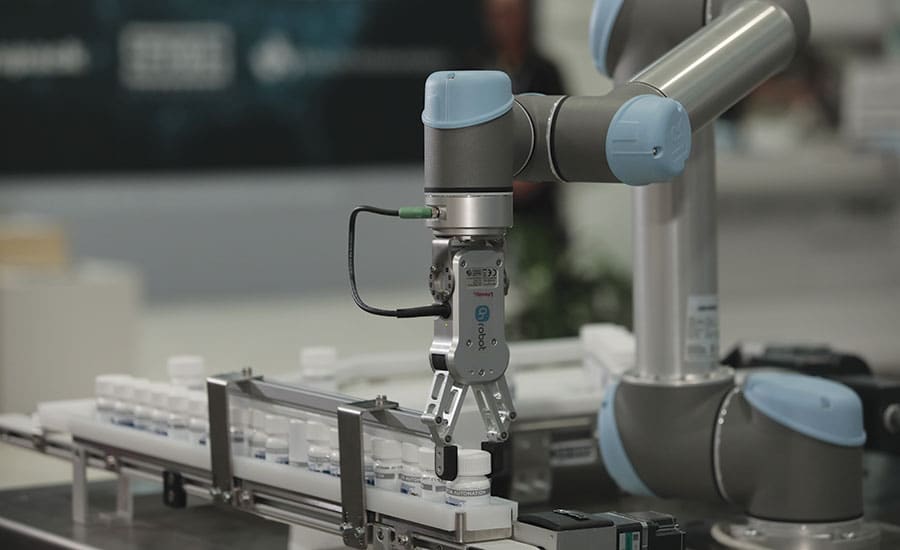
Determine object position, orientation, and alignment to guide downstream robotic or process steps. AI-driven localization handles parts presented at random angles, in cluttered bins, or partially occluded — conditions that defeat traditional template-matching vision. The resulting coordinates feed directly into robot pick-and-place, assembly verification, and precision guidance for flexible, high-mix manufacturing.
OCR
Read text or codes reliably — even on damaged, distorted, or reflective surfaces. Deep learning OCR pushes through low-contrast printing, curved surfaces, partial occlusion, and inconsistent lighting that break rule-based character recognition, verifying lot codes, expiration dates, and serial numbers at full production speed. Misreads and near-misses are flagged automatically instead of silently passing through.
Typical Applications by Industry
Fields of Application
Powered by Industry-Leading Vision Technology
Systech Technology
Global leader in serialization, authentication, and track-and-trace solutions for pharmaceutical and consumer goods industries. We deploy Systech UniSeries software for end-to-end product serialization, aggregation, and regulatory compliance across packaging lines.
Cognex
World leader in machine vision and industrial barcode reading. We deploy Cognex In-Sight vision systems, DataMan barcode readers, and VisionPro deep learning tools for the most demanding inspection applications.
Zebra Technologies
Industry leader in fixed industrial scanning and machine vision. We integrate Zebra's fixed scanners, smart cameras, and Aurora Vision software for high-speed inspection and data capture on production lines.
SICK Inc.
Global leader in sensor intelligence and industrial vision. We deploy SICK's 2D and 3D vision cameras, LiDAR sensors, and Inspector vision systems for quality inspection, measurement, identification, and guidance applications across manufacturing and logistics environments.
Keyence
Global manufacturer of machine vision systems, code readers, and sensors. We integrate Keyence vision systems and code readers for inspection, measurement, and part identification on production lines.
From Assessment to Production
Vision Assessment
Our machine vision integrator team analyzes your product, defect types, line speed, and environment to determine the optimal camera, lighting, and algorithm approach for your automated optical inspection needs.
System Design & Proof of Concept
Our engineers design the industrial machine vision system, select optics and lighting, develop inspection algorithms, and validate detection rates with sample products for your vision system integration.
Vision System Integration
We install cameras, lighting, and enclosures on your line, integrate with PLCs and reject mechanisms, and commission the automated optical inspection system to production standards.
Validation & Optimization
Production validation confirms detection rates, false reject rates, and cycle times. Our machine vision integrator team fine-tunes algorithms and trains your operators for ongoing inspection success.
Full Stack Automated Serialization System
Pharmaceutical Manufacturing
- 24/7 Fully Serialized Packaging Line
- 99.9% Serial Number Database Reliability
- Full DSCSA Compliance for Global Distribution
Explore Related Services
Advanced Robotic Applications
Robotic cell design, FANUC robot programming, palletizing, machine tending, and cobots.
Learn moreSorter Conveyors & Material Handling
Conveyor design and installation, automated sortation, inspection tunnels, and WMS integration.
Learn morePLC Panel Building & Programming
PLC programming, control panel building, HMI and SCADA, and commissioning.
Learn moreRelated case studies: Sorter Conveyor with Tunnel Inspection System
Common Questions About Machine Vision Integration
Ready for Automated Optical Inspection?
Schedule a free vision assessment with our machine vision integrator team. We'll evaluate your inspection challenges, demonstrate automated optical inspection capabilities with your actual products, and provide a detailed proposal for your vision system integration.
Schedule Free ConsultationNo commitment required. We'll respond within 24 hours.